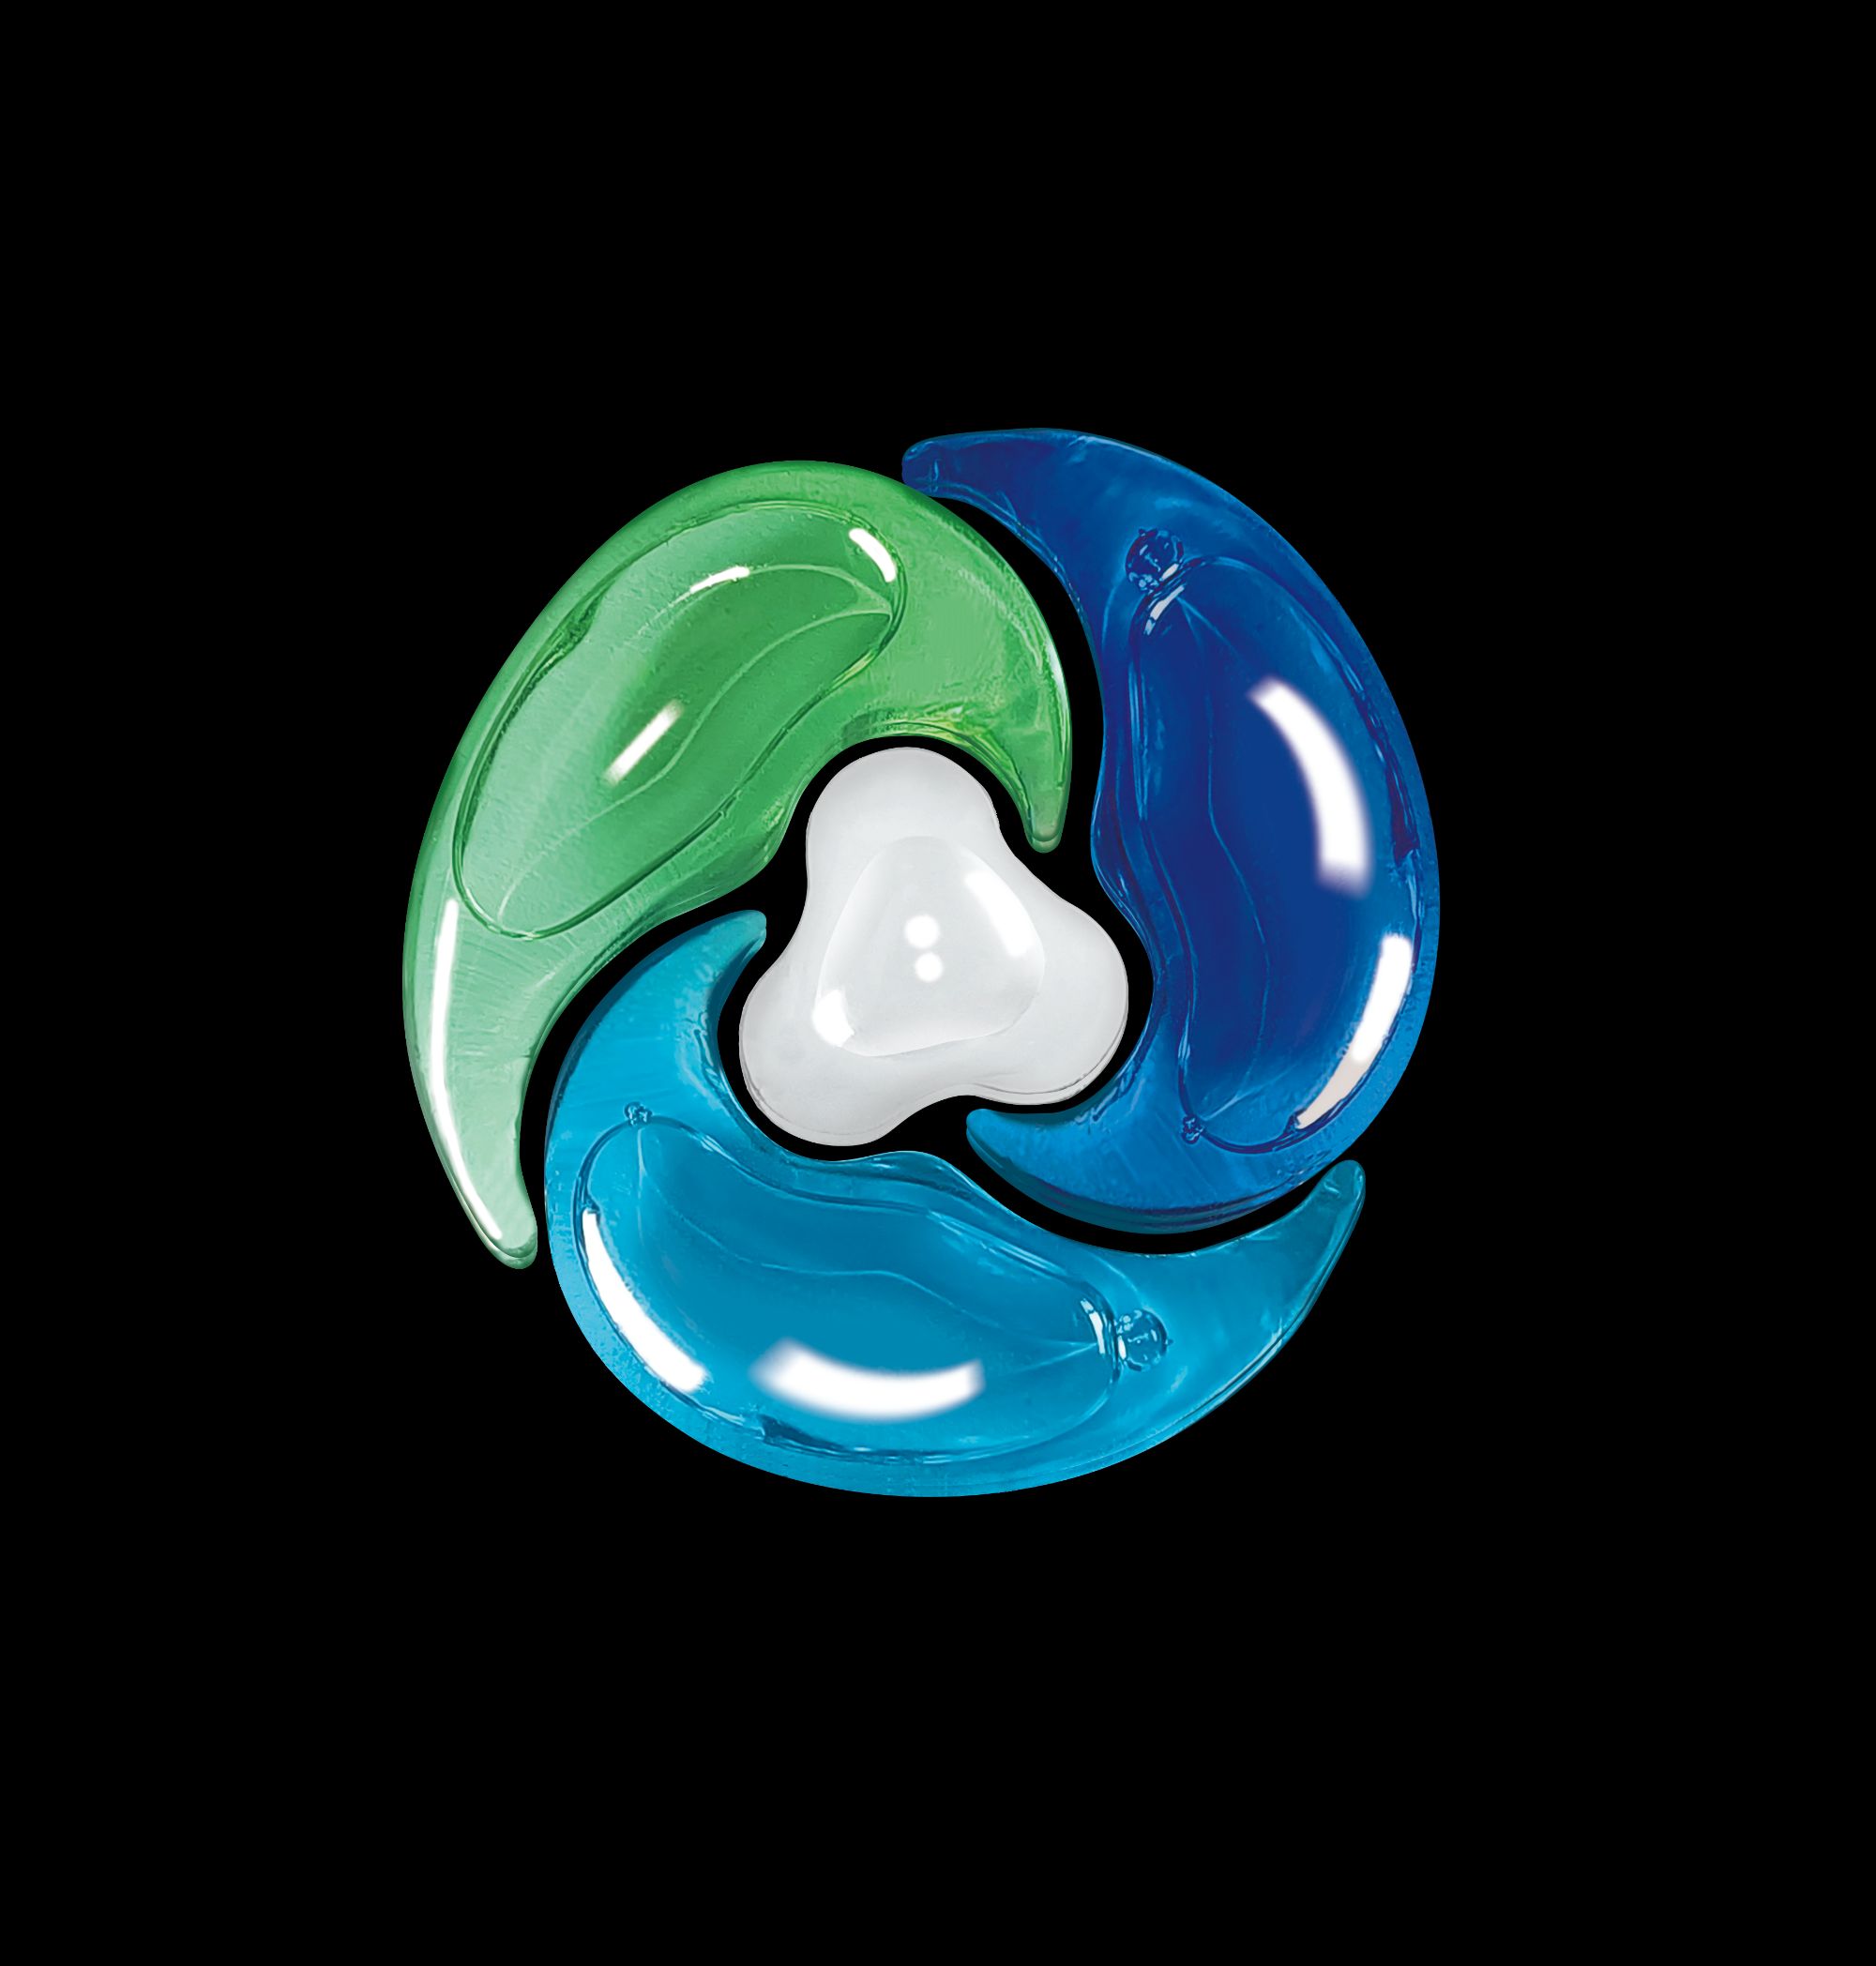
4 Chamber Laundry Pods Exporter Checklist for Quality and Compliance
2026-11-02
Navigating the booming global market for laundry pods? If you're exporting 4-chamber pods, quality and compliance aren't just boxes to tick—they're your ticket to customer trust and repeat orders. Yet with shifting regulations and rising buyer expectations, where do you start? That's where LANJIEYA's hands-on checklist comes in. In this post, we break down the must-check essentials—from formulation stability to packaging integrity and documentation—so you can ship with confidence, not guesswork.
Raw Material Vetting That Catches Contamination Early
Every incoming batch tells a story before it ever reaches the production line. We dig into supplier records, shipping conditions, and visual cues that hint at contamination risks most teams overlook. A slight color shift in a resin sample or an off-spec moisture reading isn't just a data point—it's a red flag that gets investigated on the spot.
Instead of relying on a single screening method, our vetting combines rapid spectroscopy, melt flow indexing, and targeted microbial swabs. The goal isn't to reject more material; it's to catch the subtle failures that slip through standard checks. One contaminated pallet can shut down a line for days, so we treat every shipment as a potential weak link until proven otherwise.
What sets this apart is the feedback loop with our suppliers. When a batch shows early signs of cross-contamination, we don't just quarantine it—we trace the root cause back to the source, often within hours. That means fewer rejected lots overall, because suppliers adjust their handling before problems become recurring patterns.
The Certifications Customs Agents Actually Look For
A valid customs broker license is the first thing that gets checked, but it's rarely enough on its own. Agents pay closer attention to whether the broker or forwarder holds active C-TPAT membership, especially for shipments moving through U.S. ports. That certification signals a documented supply chain security program, which can cut down on exam rates and keep cargo from sitting in limbo.
Beyond the basics, things like IATA accreditation for airfreight and AEO status for European clearances carry real weight. If you're shipping perishables or pharmaceuticals, expect the agent to verify specific handling certifications rather than just accepting a generic freight forwarder badge.
Packaging That Survives Humidity and Rough Handling
Cardboard boxes won't cut it when moisture seeps into the supply chain. The right packaging starts with high-density polyethylene (HDPE) liners or coated corrugated boards that block water vapor before it reaches the product. These materials don't just resist dampness—they shrug off condensation, sudden rain, and even accidental splashes during transit. Look for sealed seams and overlap flaps that prevent liquid from sneaking through the corners, where most failures begin. For extra protection in tropical climates, add a desiccant pouch inside each carton, but make sure the outer layer can stand on its own without relying on humidity indicators.
Rough handling is where packaging gets brutalized—dropped from conveyor belts, stacked too high, or kicked across warehouse floors. A durable shell needs more than thick walls; it needs structural geometry that spreads impact forces. Double-wall corrugated board with fluting oriented vertically absorbs vertical compression, while edge protectors made from recycled plastic or reinforced fiberboard shield the weakest points. Strapping with polymer banding instead of steel reduces the risk of cutting into the carton while still holding heavy loads tight. Test every design by simulating a six-foot drop onto concrete and a forklift clamp squeeze before approving it for shipment.
But survival isn't just about material specs—it's about anticipating the messiest scenarios. Think of a pallet left on a loading dock during a thunderstorm, or a courier tossing a package over a fence. Combine moisture barriers with impact-resistant corners and non-slip coating on the bottom to keep stacks stable. For long-haul ocean freight, use vented yet waterproof membranes that equalize pressure without letting humidity in. The best packaging feels over-engineered because it has to be: one split seam or soggy wall can compromise the entire shipment, and no one wants to explain that to a customer.
Pre-Shipment Dissolution and Leak Tests Worth Running
Dissolution failures found after shipping are a quiet disaster. A pre-shipment dissolution test doesn't need to be exhaustive; it needs to be representative of the batch's worst case. For immediate-release tablets, testing three time points (usually 5, 15, and 30 minutes) with a full media pH range often catches a poor disintegrant blend or an unnoticed change in granule hardness. For modified-release products, run the full profile on the oldest and youngest samples from the line, since dwell time can subtly alter release rates.
Leak testing is equally case-specific. Vacuum decay works well for rigid bottles and glass vials, but flexible pouches need either dye penetration or a pressure differential method that won't crush the pack. Blister packs respond best to a combination of a visual cold-seal check and a methylene blue immersion under vacuum; just make sure the vacuum cycle doesn't create false positives by pulling product dust into the channel.
The tests worth running are the ones tied to known failure modes in your packaging line. If you've never had a cap liner leak, skip the helium test and spend the effort on a 100% torque check instead. If your product is hygroscopic, a short-duration water vapor transmission challenge on sealed bottles is more valuable than a 24-hour dye bath. The goal isn't to test everything; it's to catch the defect that would otherwise reach a patient.
Export Documentation That Won't Trigger Hold Notices
Mismatched details across shipping documents are one of the fastest ways to get a container flagged. A misspelled consignee name on the bill of lading versus the commercial invoice, or a weight discrepancy of even a few kilograms between the packing list and the carrier's manifest, can prompt customs to set your shipment aside for manual review. Before submitting anything, run a fresh cross-check on every numeric field and proper noun. Better yet, have a second person with no prior involvement in the file do the review—fresh eyes catch typos that the original drafter's brain automatically corrects.
Vague product descriptions invite scrutiny. Terms like "parts," "gifts," or "general merchandise" tell a customs officer nothing about what is actually inside the cartons, and they often trigger a request for clarification that adds days to clearance. Write the description exactly as it appears in the harmonized system code, then match that wording across the invoice, packing list, and certificate of origin. For example, "stainless steel hex bolts, metric M8 x 30, grade A2-70" will sail through far more smoothly than "metal fasteners." If you are shipping a mixed consignment, break out each commodity line separately rather than lumping everything under one heading.
Destination-specific paperwork gaps are another common hold-up. Some countries demand a consular invoice, a particular type of certificate of origin, or an import permit that your standard document set does not include. These requirements change more often than most exporters realize, so confirm them with the buyer or their freight forwarder at least a week before the vessel sails. Keep digital copies of every submitted document—including any amendments—so that if a customs officer asks for a clarification, you can respond within hours instead of days, keeping the clearance clock moving.
Factory Audits Beyond the Surface-Level Walkthrough
Most factory audits stop at the first impression—clean floors, a well-organized warehouse, and a production line humming along. But those surface signals rarely tell you anything about what happens when the auditor leaves. A meaningful audit digs into the systems that only reveal themselves under pressure: how batch records are maintained at 2 a.m., whether corrective actions from last year’s nonconformities actually stuck, or why a quality manager suddenly goes quiet when asked about supplier traceability. That’s the gap between a checkbox tour and a real operational assessment.
Beyond the walkthrough, you need to test the factory’s reflexes. Pull a random lot from the quarantine area and trace it backward through raw material logs, maintenance schedules, and operator training records—without giving the team time to prep. Watch how the line handles a simulated defect: does the operator stop and flag it, or quietly rework it to keep the output numbers green? Check whether night-shift supervisors have the same authority to halt production as their daytime counterparts. These are the moments where process discipline either holds or collapses, and they’re invisible from the visitor’s path.
Finally, separate the factory’s documented policies from its unspoken habits. Ask the floor team—not just management—what happens when a machine drifts out of tolerance. Compare their answers to the official SOP. If there’s a shrug, a laugh, or a “we have a workaround for that,” you’ve found something more important than any audit checklist item. Real capability doesn’t live in the binder on the conference room table; it lives in the split-second decisions people make when they think no one is scoring them.
FAQ
Verify surfactant blend percentages, enzyme activity levels, pH of each chamber solution, dye and fragrance allergen content, and confirm all ingredients meet EU Detergent Regulation or destination market restrictions.
Perform compression and drop tests per ISTA 3A, then use a water immersion leak test at 40°C for 24 hours to detect micro-leaks. Also measure film tensile strength after accelerated aging.
For EU, ensure compliance with CLP and Detergents Regulation, plus biodegradability test results. For North America, provide SDS and child-resistant packaging certification to CPSC standards.
Run dissolution tests in water at 15°C, 30°C, and 60°C with both hard and soft water. Record time for full chamber film dissolution and ensure no residue remains after a standard 30-minute cycle.
Include hazard pictograms per GHS, ingredient disclosure per region, dosage instructions with four-chamber graphic, and warnings like "Keep out of reach of children" in required languages. For the EU include UFI code.
Request process capability data for fill weight per chamber (Cpk > 1.33), verify inline checkweigher records for each cavity, and conduct random destructive testing to measure actual fill volume against spec.
Use moisture-barrier film like PET/AL/PE laminate for primary pouches, add desiccant sachets in secondary cartons, and validate closure integrity via vacuum leak testing after conditioning at 90% RH for 72 hours.
Provide real-time and accelerated stability data (40°C/75% RH for 6 months) showing chamber film integrity, fragrance retention, and enzyme activity remaining above 90% of label claim.
Conclusion
For any exporter shipping four-chamber laundry pods, the real work starts long before the containers leave the dock. Too many suppliers treat raw material checks as a formality, yet a single contaminated surfactant batch can force a full recall once customs runs its own lab tests. Vetting every incoming lot for heavy metals, microbial load, and unexpected polymer residues isn't just about passing an audit—it's about catching the kind of contamination that ruins a buyer relationship. At the same time, the certifications that actually matter at the border are not generic ISO prints. Customs agents look for REACH compliance, EU Detergent Regulation documentation, and often a specific biodegradability test report. If those papers don't match the exact product formulation, expect a hold notice, not a handshake.
Packaging is where many export batches fail quietly. Four-chamber pods sit in humid shipping containers for weeks, and if the film doesn't hold up, you get leakers that dissolve into a sticky mess before the pallet reaches the warehouse. Pre-shipment dissolution and leak testing should be done on samples pulled from the actual production line, not lab-made prototypes—run them at the same temperature and humidity they'll face in transit. And don't assume your export docs are fine because your domestic ones are. A missing SDS update or an incorrect HS code on the commercial invoice can trigger an automatic hold that costs more in demurrage than the whole shipment's margin. Finally, factory audits need to go beyond the showroom. Watch how workers handle rejected raw materials, check whether cleaning logs match actual production schedules, and ask to see the last three corrective action reports. That's where the real compliance picture lives.
Contact Us
Contact Person: Zhao Yanlong
Email: [email protected]
Tel/WhatsApp: 8615832007309
Website: https://www.gzlanjieya.com